Capsule House Factory Quality Control: Buyer Guide
Capsule house factory quality control: five stage gates from frame to final test, what to check before the envelope closes and which records to require.

Most buyers meet quality control once, at the end, in the form of a pre-delivery inspection. By then it is too late to influence anything: the lining is closed over the insulation, the services are buried, the glazing is set. Useful quality control on a factory-built unit happens during production, at a small number of stage gates where a defect is still cheap to correct. This page sets out those gates for a capsule house order, what is checked at each, and what record to request. The once-off supplier audit is covered in the factory audit checklist, the end-of-line inspection in pre-delivery inspection, the reference-unit gate in sample unit approval, and general supplier selection in how to choose a capsule house manufacturer.
Why stage gates rather than a final inspection
A volumetric unit is assembled in a sequence, and each step covers the one before it. Insulation is covered by lining, services are covered by finishes, sealant is covered by trim. Once a step is closed, verifying it means destructive opening, and correcting it means rework that touches finished work.
That creates a simple principle: inspect at the last moment each element is still visible. Everything else — how many inspectors there are, what the final checklist looks like — matters much less than whether the gate timing is right. A buyer who attends one gate at the right moment catches more than a buyer who attends five at the wrong ones.
Gate 1: frame and dimensional check
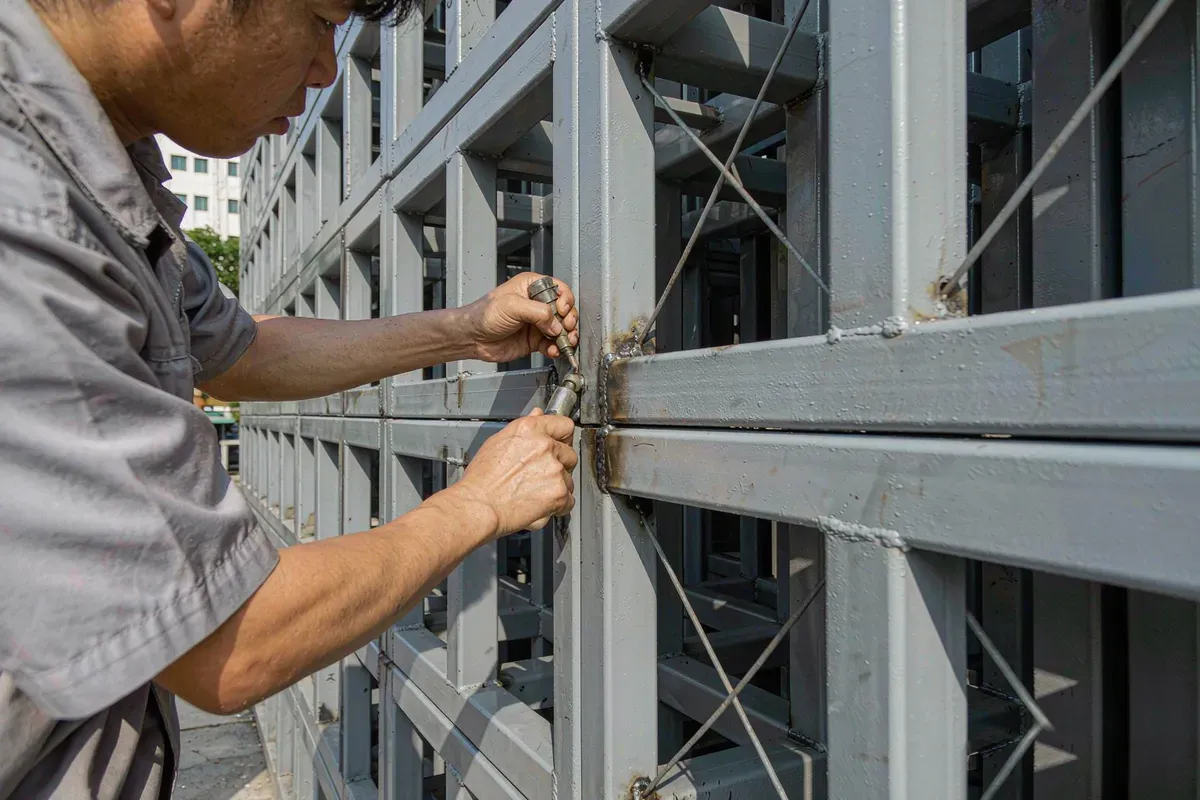
The frame determines everything that follows. If it is out of square or out of dimension, the lining, the glazing and the joinery will all be forced to absorb the error, and they will show it.
- Overall dimensions against the approved drawing, at several points rather than one.
- Diagonal measurements to confirm squareness.
- Weld condition at visible seams: consistency, penetration, spatter removal, and any undercut.
- Corrosion protection: preparation, coating coverage, and any damage that needs repair before it is covered.
- Lifting and tie-down points: present, correctly located, and reinforced as drawn.
- Material identification against the specification, where the order states a grade or section.
Ask for the dimensional record, not just a verbal confirmation. A signed sheet with actual measurements is the artefact that resolves a later dispute about whether a tolerance was met.
Gate 2: envelope, before it is closed
This is the gate most often missed and the most valuable. Once the internal lining is fixed, the insulation layer can no longer be verified without opening it.
| Element | What to verify while visible | Defect that appears later if missed |
|---|---|---|
| Insulation | Coverage with no gaps, correct thickness, no compression, no voids at corners | Cold spots, condensation lines, higher running cost |
| Vapour control layer | Continuity, correct side for the intended climate, sealed laps and penetrations | Interstitial condensation and a musty interior that is hard to diagnose |
| Air barrier | Sealed at junctions, service penetrations and openings | Draughts, moisture ingress and heating or cooling underperformance |
| Thermal bridges | Treatment at posts, ring beam and any steel penetrating the layer | Visible lines on the internal surface and local condensation |
| Fire and acoustic provisions | Present as specified, correctly positioned, not displaced by services | A compliance question that cannot be answered after closing |
Photograph this gate comprehensively and label the photographs by unit number and location. In a dispute about what was inside a wall, photographs taken at the right moment are the only evidence that carries weight.
Gate 3: services rough-in and pressure test
Services are installed before finishes, and that is the moment to test them. Water should be pressure tested to the specified test pressure and held, with the result recorded. Drainage should be checked for fall and for leaks. Electrical work should be tested for insulation resistance, polarity and earth continuity, again with recorded values rather than a pass statement.
Confirm that what is installed matches the load schedule agreed at order stage. A unit destined for a hot climate with air conditioning, a water heater and a kitchen has a materially different electrical provision from one that does not, and the difference is invisible once the finishes are on.
Gate 4: glazing, wet areas and water test
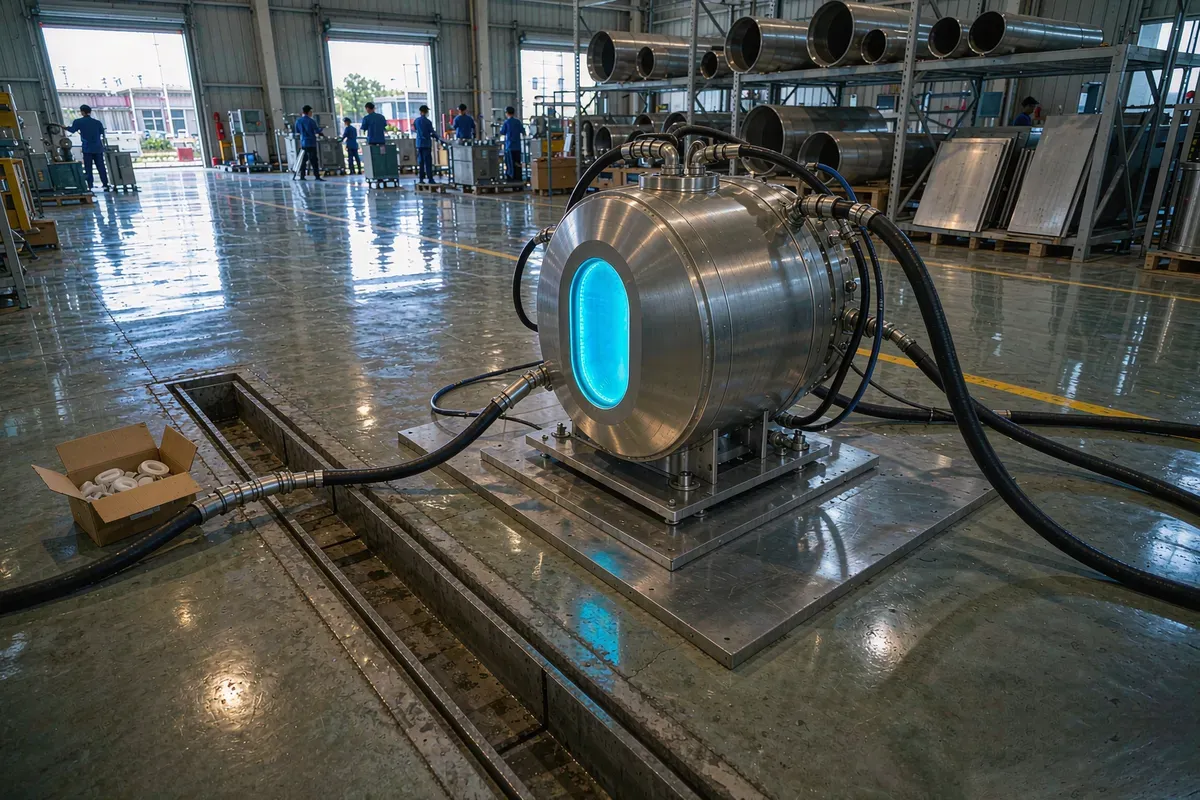
Water ingress is the defect most reported by owners and the one most preventable in the factory. Two tests matter.
Glazing: setting blocks, frame fixing, gasket continuity and sealant application, followed by a water application over the sealed perimeter with an inspection from inside. Wet areas: tanking or waterproof membrane continuity, upstands at junctions, floor falls to the drain and the drain connection, followed by a flood or spray test with the result recorded.
Then a whole-unit water test. Whether this is a spray rig, a hose application or another method depends on the facility, but it should be done, done long enough to be meaningful, and followed by an internal inspection. A leak found in the factory is a sealant repair. The same leak found after installation is a logistics problem, a schedule problem and a relationship problem.
Gate 5: finishes, and final electrical test
Finishes are where the defect is cosmetic but the dispute is real, because finish standards are subjective. The reference unit approved under the sample process is what makes this objective: compare to the approved sample, not to an expectation. The sample gate and how the approved unit becomes the reference for the batch are described in sample unit approval.
The final electrical test should repeat the rough-in tests on the completed unit, because fixtures fitted after the first test can introduce faults. Add functional testing: every luminaire, every socket, every switch, every appliance, the door and window hardware, the locking, the ventilation and any monitoring or control device. A functional run-through with a checklist catches more than a visual inspection, particularly for items that were specified as options.
Records to request at each gate
Agree the documentation set at order stage. Requesting it at the end is how buyers discover it was never produced.
- Dimensional record with actual measurements, signed and dated.
- Envelope photographs, before closing, referenced to unit number and location.
- Pressure test result for water services, with test pressure and holding time.
- Electrical test results: insulation resistance, polarity, earth continuity.
- Water test record, with method and duration, and the internal inspection result.
- Material certificates or declarations where the order specifies a material or component.
- A deviation log: anything that differs from the approved sample or drawing, with the reason and who accepted it.
The deviation log is the one buyers forget and the one that matters most. Every unit differs slightly; the question is whether the difference was recorded and accepted, or discovered later.
Who attends, and how
Attending every gate in person is expensive and usually unnecessary. A workable arrangement for a first order is to attend the sample unit build in person or by a representative, require photographic records at each gate for the remainder of the batch, and take a live video walk-through at the pre-closing gate where the envelope is still visible. Remote attendance is now normal and most factories accommodate it.
State the arrangement in the order: which gates, what notice is required to attend, what records are provided within what period, and what happens if a gate is missed. A buyer who has contracted for the record gets the record; one who asks for it afterwards gets an explanation.
Haishu manufactures space capsule homes and expandable prefab houses to order and can agree stage-gate inspection, photographic reporting and documentation as part of the order. Any certificate, test report or compliance document should be requested explicitly and verified against the requirement of the receiving authority, rather than assumed to be included. Requirements may vary by application, market and applicable standard.
More from the Blog
Capsule Home Cost Guide: What You Really Pay in 2026
EXW, shipping, install and the hidden line items — a transparent breakdown of total landed cost.
Read article →
How to Install a Capsule Home in 3 Days: A Step-by-Step Guide
From site prep to first guest — the exact sequence our install crews follow on every deployment.
Read article →
Real Owners, Real Numbers: Success Stories
How a lakeside resort, a Spanish glamping site and a Singapore dealer hit their targets.
Read stories →Talk to the Factory
Ready to Ride the 2026 Wave?
Get the latest catalog, pricing tiers and a layout sketch for your land — straight from the engineering team.